Outdoor Paving Tiles OEM: A Complete Guide to Custom Manufacturing Solutions
2026-11-02
Finding a reliable partner for custom outdoor paving tiles can feel like a dead end—until you explore OEM manufacturing. With Beata Ceramics, you're not just buying stock tiles; you're getting a complete custom manufacturing solution built around your project's specs, finishes, and branding. This guide unpacks the full OEM process, so you can turn your outdoor tile concept into a production-ready reality without guesswork.
Why Custom Outdoor Pavers Need More Than a New Color Coating
A fresh coat of color can make faded pavers look tidy for a few months, but it does nothing for spalled edges, sinking units, or joints that have started to spread. Custom outdoor pavers usually sit in high-traffic zones and face freeze-thaw cycles, so any weakness in the bedding layer or edge restraint will keep causing movement no matter how bright the surface looks. If the base is no longer stable, the new coating simply flakes off with the first seasonal shift, and you are back to square one with an uglier patch job.
Durability also depends on what you cannot see from above: the joint sand, the drainage slope, and whether the sealer allows moisture to escape. Recoloring a dense concrete or natural stone paver can trap water vapor, leading to efflorescence, whitish haze, or small pop-outs that ruin the finish. Instead of chasing another layer of pigment, a worthwhile renewal focuses on re-leveling low spots, refilling joints with the right aggregate, and choosing a coating that preserves the paver's original grip and texture rather than just hiding the damage.
Reading Between the Lines of Factory Tolerance Claims
Factory tolerance claims often read like a promise of precision, yet the fine print tells a different story. A datasheet may boast ±0.005 mm on a machined part, but without context, that number is only half the truth. Tolerances are typically defined under ideal conditions—fresh tooling, controlled temperature, and a single measurement point. Once production variables creep in, the real spread can drift well beyond the glossy figure.
Wise engineers look past the headline number and ask harder questions: Was the tolerance verified across an entire batch or just on a golden sample? Does it hold at the extreme ends of material hardness or surface finish? Often, the quoted range disappears when the part is mounted, welded, or exposed to thermal cycling. The gap between lab data and shop-floor reality is where tolerance claims quietly unravel.
Reading between the lines means treating every tolerance as a conversation starter, not a closed case. Request the measurement report, check the Cpk value, and run your own capability study on incoming parts. The cheapest supplier with the tightest printed spec can end up costing the most when hidden variation surfaces on your assembly line.
Mold Development Timelines and the Cost of Rework
A typical mold development schedule spans anywhere from six to fourteen weeks, depending on part complexity, number of cavities, and surface finish requirements. The first two weeks are usually consumed by design reviews and steel procurement, while rough milling, heat treatment, and EDM work occupy the middle stretch. Final fitting and polishing rarely go exactly as planned. When a timeline gets compressed, corners get cut in the very stages that prevent costly mistakes later.
Rework is where budgets quietly unravel. A single dimensional change after hardening can force the shop to re-machine an insert, re-cut an electrode, or even scrap a cavity block entirely. Each iteration tacks on days or weeks, and the labor cost compounds quickly. Many molders underestimate how much rework stems from unclear part data or last-minute engineering changes, not from machining errors alone.
The relationship between timeline and rework is rarely linear. Shaving a week off the front end often adds three weeks of corrections after the first trial shot. Shops that hold design freeze dates and invest in upfront DFM analysis tend to deliver on time with fewer emergency tooling changes. In mold development, slow is frequently faster and almost always cheaper when rework is counted honestly.
Batch Testing Protocols That Catch Outdoor Failures Early
Pull ten units from every production run, not just the first five. Send them through a forty-eight-hour salt spray chamber, then a thermal shock cycle from -20°F to 120°F before any load testing. The failures that matter rarely show up in a single stress pass.
Record exactly where each sample breaks—zipper tracks, seam tape, buckle pins—and compare that against the previous batch's failure map. A shift of more than two points in the same location usually means a supplier changed something without telling you. Catch it here, not on a ridge line.
Finally, run one wet-out test with actual field dirt, not lab-grade dust. Pack a stuff sack, leave it in a rain barrel for six hours, then check the waterproofing. It is not elegant, but it exposes the kind of slow leak that warranty claims are made of.
How Aggregate Grading Influences Freeze-Thaw Survival
In freeze-thaw exposure, the physical arrangement of aggregate sizes sets the stage for how much water the concrete can hold and how easily it can move. A continuous, well-graded aggregate packs tightly, leaving fewer interconnected voids in the skeleton. This does not automatically guarantee durability—air voids still do the heavy lifting—but it lowers the volume of large, water-filled channels that feed ice growth. Poorly graded or gap-graded mixes, by contrast, often leave larger gaps between particles. Those gaps demand more mortar to fill, and if that mortar lacks a proper air-void system, it becomes a network of vulnerable capillaries.
Grading also shifts the balance between coarse and fine particles, which changes permeability and the distance water must travel before it reaches a free surface. Finer blends create tortuous pathways that slow saturation but can trap moisture once it gets in. Coarser, more open gradings drain faster, yet they may increase localized stress where ice forms in larger pores near aggregate boundaries. The key is not just density but the pore size distribution: a well-graded mix tends to produce a finer, more uniform capillary network, which helps keep individual ice lenses small.
Perhaps the most overlooked influence is how grading affects the interfacial transition zone. When aggregates are too uniform or too coarse, excess paste collects around particles, and that paste shrinks and cracks more readily under thermal cycling. These microcracks draw in water and accelerate freeze-thaw damage from the inside out. By adjusting the proportion of mid-size particles, a mix can reduce paste pooling and distribute stress more evenly, giving the concrete a better chance of surviving hundreds of cycles without scaling or spalling.
OEM Contracts and the Ownership of Your Custom Designs
When you engage an OEM partner to manufacture your custom designs, the contract you sign becomes the single most important document for determining who ultimately owns the product's intellectual property. Too many brands assume that paying for tooling or providing CAD files automatically transfers ownership rights. In reality, unless the agreement explicitly assigns design ownership, copyright, and any resulting patents to your company, the factory may retain significant claims—especially if they contributed engineering refinements or production-ready modifications during the development process. A well-drafted OEM contract should address not only the final goods but also every intermediate file, mold, prototype, and proprietary technique that emerges along the way.
A common pitfall is treating the OEM agreement as a simple purchase order with added quality clauses. Custom design ownership requires clear language about derived works: if the manufacturer suggests a material substitution or a structural tweak to improve moldability, who owns that improvement? Without a clause stating that all modifications, derivative designs, and manufacturing know-how developed for your project become your exclusive property, the factory can later argue that their contributions form a separate, jointly owned or factory-owned body of work. This becomes critical when you later switch suppliers or try to enforce exclusivity against a competitor using the same OEM partner.
Before signing, map out every tangible and intangible asset tied to your design—3D models, engineering drawings, logo files, color specifications, packaging dielines, even the configuration of the production line. Then confirm that the contract grants you irrevocable, worldwide ownership of these assets, along with the right to retrieve all physical and digital copies upon termination. If the OEM insists on retaining any rights, negotiate a narrow license limited to manufacturing your specific orders and nothing else. Protecting ownership at the contract stage is far cheaper than trying to recover your designs through litigation after a relationship sours.
FAQ
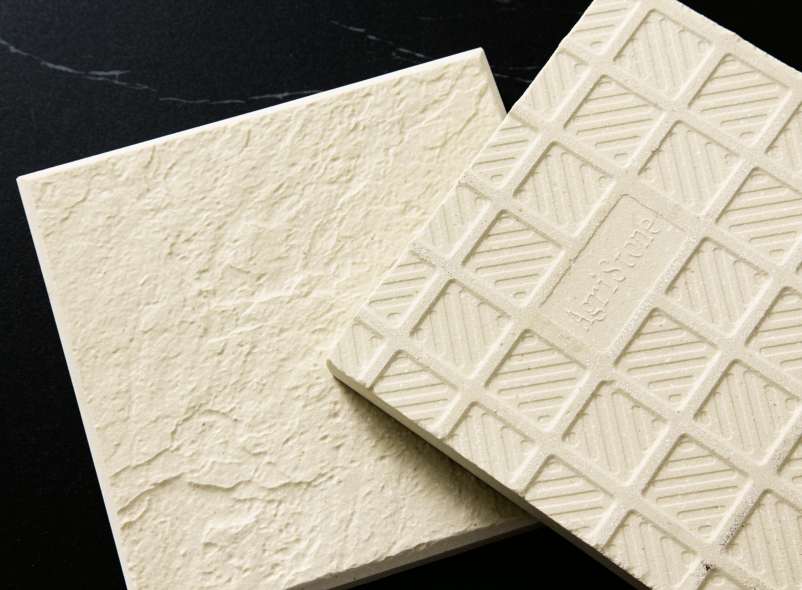
OEM means the factory manufactures tiles to your own specifications — not their existing stock. You can define the exact dimensions, edge profile, surface texture, color mix, and even the type of packaging. This is a different game from picking a standard 600x600mm tile off a shelf. For outdoor work, custom OEM often makes sense when you need to match an existing patio, hit a specific R11 slip rating, or create a unique stone-like finish that retail products don't offer.
It usually starts with a technical drawing or reference sample, followed by a mold design and a first sample run. After you approve the sample, the factory moves to a small trial batch so you can check size consistency and surface finish. Only then does full production begin. Depending on the complexity, this can take anywhere from four to eight weeks. The key is to request a pre-production sample from the actual production line, not a hand-finished prototype, so there are no surprises later.
Concrete is the most flexible for OEM because you can adjust aggregate, pigments, and surface treatments easily. Natural stone like granite or limestone gives a premium look but custom cutting and finishing are more expensive. Porcelain is great for low water absorption and frost resistance, though the mold costs are higher. For high-traffic public areas, I'd lean toward concrete with a hard-blasted or bush-hammered texture; for a high-end residential patio, porcelain or sawn granite might be worth the extra cost.
Ask to see their mold-making facility and color lab, not just photos of finished projects. A solid factory will have in-house CNC mold engraving and a spectrophotometer for color matching. Request a set of 3-5 physical samples with the exact same texture depth and pigment ratio you need. If they can't explain how they control aggregate exposure or how they prevent edge chipping during demolding, that's a red flag.
For custom concrete tiles, MOQs often start around 500 to 1,000 square meters because the mold and setup costs are amortized over the whole run. Natural stone and porcelain may have lower or higher minimums depending on the factory. The biggest cost drivers are mold creation, number of different sizes, special aggregates or pigments, and any secondary process like flaming or tumbling. If you can stick to one or two sizes and one finish, you'll keep the per-square-meter price much more reasonable.
Specify the performance standards you need, like a maximum water absorption of 3% for concrete or 0.5% for porcelain, and ask for third-party test reports for freeze-thaw resistance and breaking load. For UV stability, use iron oxide pigments rather than organic dyes. If the tiles will carry vehicles, require a minimum compressive strength — usually 50 MPa or higher for concrete. Don't rely on the factory's word; ask for the actual test data from an accredited lab.
The biggest mistake is approving a sample without seeing the full production mold, which can lead to slightly different edge details or texture depth. Another is not documenting tolerances — length, width, thickness, and flatness should be agreed in writing, typically within ±1 mm for refined tiles. Also, people often forget about packaging and palletizing requirements for outdoor storage, which can cause chipping during transport. Write everything into the production order sheet, including the acceptable range of color variation.
Yes, most reputable factories offer prototype or sample batches, usually 2 to 10 square meters. You'll need to cover the mold cost and a setup fee, but this is the only way to check the real surface texture, color against your design intent, and edge quality under production conditions. Request both a dry and wet photo of the samples, and if possible, have them shipped on a small pallet rather than loose in a box to see how they travel.
Conclusion
Custom outdoor paving tiles often fail not because of the color layer, but because the entire manufacturing process was never truly adapted to the outdoor environment. A fresh coating might hide surface issues for a season, yet the real problems—weak aggregate bonding, improper curing, or a mold design that ignores thermal movement—will resurface. Savvy buyers read beyond factory tolerance claims, asking for actual measurement reports from multiple batches rather than a single ideal sample. Mold development timelines matter too: rushing a mold means you pay for rework later, when a slightly longer prototyping phase could have corrected edge profiles and joint spacing before production. Without early batch testing protocols that simulate freeze-thaw cycles, water absorption, and load stress, you won't catch a failing tile until it's already installed outside.
Aggregate grading is the quiet architect of freeze-thaw survival. If the stone particles are poorly distributed, voids trap water that expands in cold weather, splitting the tile from within. A reliable OEM partner adjusts sieve curves for your specific climate and traffic level, not just for the cheapest mix. Equally important is the contract itself: many buyers discover too late that they don't own the custom mold or the surface texture design, locking them into a single factory for reorders. Negotiating clear ownership and transfer rights from the start prevents costly redesigns and supply chain surprises. In short, a complete custom paving solution blends honest material science, patient process control, and contractual clarity—not marketing gloss.
Contact Us
Contact Person: Emma
Email: [email protected]
Tel/WhatsApp: 8618064423698
Website: https://www.beataceramics.com/