OEM Tactile Switches Factory: How to Choose the Best Custom Manufacturing Partner
2026-11-02
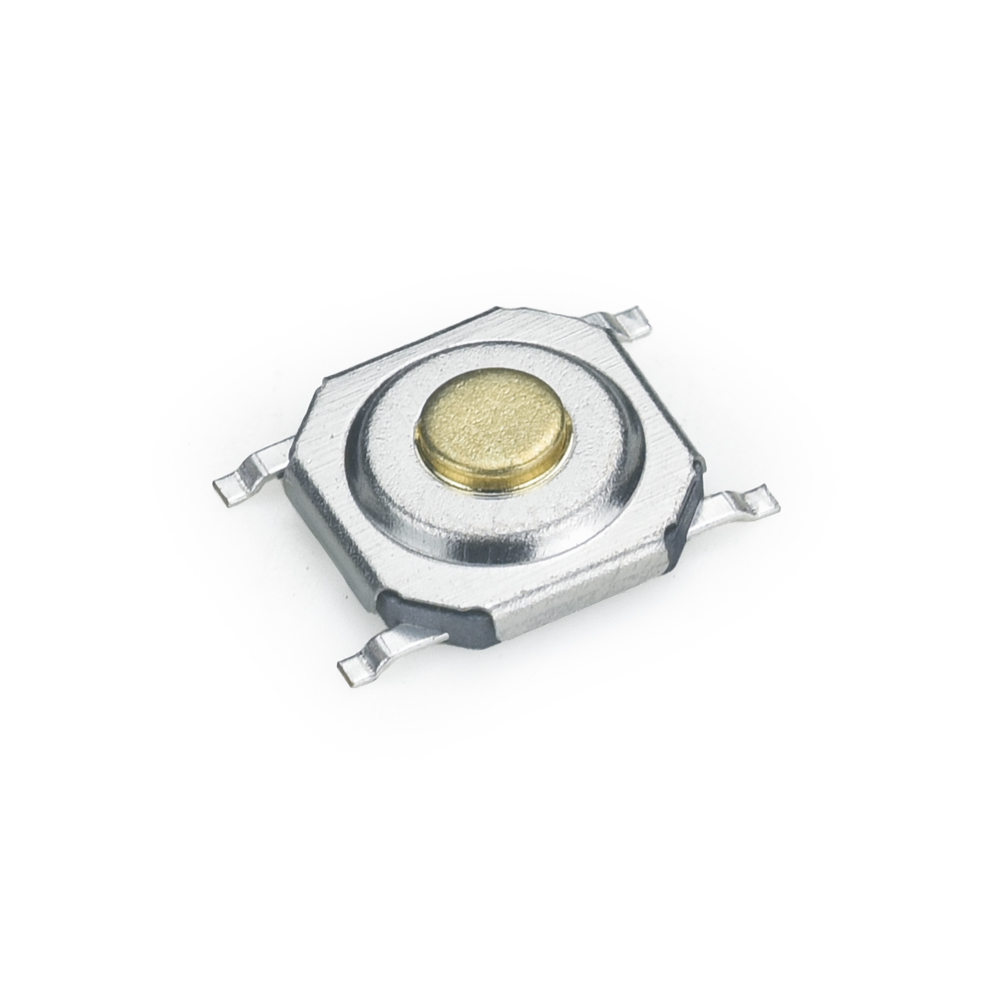
Finding an OEM tactile switches factory that actually understands your product's feel, lifespan, and integration constraints is harder than most spec sheets suggest. KEJIAN ELECTRONICS has spent years turning those vague 'good quality' requirements into repeatable, testable manufacturing steps—and this guide unpacks what to look for before you commit to a partner.
Look Past the Catalog for Real Customization Depth
A catalog can show dozens of colorways, sizes, or modular add-ons, but that's surface-level choice. Real customization depth sits in the areas that rarely make the brochure: how a manufacturer reworks load paths, tolerances, or firmware logic to match a specific operating environment. A supplier who only tweaks a finish isn't offering depth; they're offering variety. Depth means the design team can talk through trade-offs in material grade, thermal behavior, or connector placement without defaulting to a fixed spec sheet.
Ask for the revision history of a similar project. If a vendor can walk you through why they moved a mounting boss by three millimeters or swapped a bearing type after field testing, that's a signal the catalog isn't the ceiling. The best customization partners treat the printed options as a starting point, not a boundary. They'll push back on assumptions, propose configurations that aren't listed, and document the reasoning behind each change rather than hiding behind a part number.
Prototype Speed Tells You How They Solve Problems
You can learn a lot from how quickly someone turns an idea into a working prototype. Some people need to sketch, debate, and refine the concept in their head for hours before touching a tool. Others jump straight into building a sloppy but functional version within minutes. The pace itself isn't good or bad—it's a window into their cognitive style. Fast prototypers tend to treat mistakes as cheap and reversible, so they'd rather fail early and adjust. Slower ones often feel the weight of each decision and want to minimize rework before committing. Neither approach guarantees better outcomes, but the speed tells you where their comfort zone lies.
In team settings, this becomes even more visible. When a problem lands on the table, watch who starts rearranging existing components and who opens a blank canvas. A quick prototype might be held together with tape and assumptions, but it forces the group to react to something concrete. It exposes hidden constraints, missing information, and conflicting priorities that no amount of abstract discussion would surface. The person who builds fast isn't necessarily careless; they're using the prototype as a question, not an answer. That distinction matters more than the polish of the thing they produce.
There's also a difference between speed born from experience and speed born from impatience. An experienced maker can rush because they already know which parts are likely to break and which details can wait. Impatience, on the other hand, skips steps without understanding the cost. If you watch closely, the way someone handles a fast prototype—what they choose to include, what they deliberately leave out, how they talk about its flaws—reveals how they frame the problem itself. Some people solve by narrowing scope until the core works. Others solve by expanding until something sticks. Prototype speed doesn't just show how fast they move; it shows which direction they think the solution lies.
Pin Down Tooling Ownership Before You Commit
Tooling costs can quietly spiral when nobody has claimed responsibility for the physical assets. Before you sign off on a mold or fixture, get the ownership terms in writing—who pays for maintenance, who holds the title if the project stalls, and what happens to the tool if you switch suppliers. Without this, you're essentially funding someone else's production line.
A simple line in the contract isn't enough. Ask your vendor where the tool will be stored, whether it can be moved if you need a second source, and how you'll reclaim it if the relationship ends. If they dodge the question or offer vague guarantees, treat that as a warning sign, not a negotiation detail to revisit later.
Go Beyond Certificates to See Actual Quality Checks
Certificates look tidy in a folder, but they rarely tell you whether a supplier caught a dimensional drift before shipment. We ask to see the inspection logs, the rejected batch reports, and the notes from the line supervisor. That is where quality either holds or quietly slips.
On one visit, a vendor showed us a glowing ISO audit summary while their incoming material checks had been skipped for three weeks. The paperwork was perfect; the receiving area told a different story. We now walk the floor, compare the actual measurement data against the drawing tolerances, and watch how nonconforming parts are quarantined. Real assurance comes from routine checks that happen when no one is watching, not from framed credentials on the wall.
Communication Rhythm Exposes a Factory's True Culture
Walk through any factory floor at shift change and you'll hear it before you see it: the clipped status updates, the half-finished sentences picked up by the next crew, the pause that tells an operator whether a problem is trivial or worth stopping the line. In high-trust cultures, those exchanges happen face-to-face, with names and numbers, not just ticket IDs. People don't wait for the daily standup to raise a concern; they grab a supervisor mid-stride because the rhythm of communication has already made that normal.
Contrast that with a plant where every message routes through a portal or a laminated escalation chart. The same machine hiccup triggers a different beat: log it, wait for review, forward to the right inbox. That lag isn't just inefficiency—it's a cultural signature. When workers stop talking across shifts and start composing carefully worded reports, the real message is that candid, messy, immediate conversation isn't valued. The silence between updates says more than the metrics on the dashboard.
The most revealing moments are the unscripted ones. A veteran operator leaning over to a new hire with a quick correction, a team lead who stops a huddle to ask “what are we actually trying to fix here?” These are not in any playbook. If they happen naturally, the communication rhythm is healthy. If they only happen when a manager schedules a “listening session,” the culture is already performing communication rather than living it.
Test Their Ramp-Up Plan Before Scaling Gets Chaotic
Most founders treat a ramp-up plan like a checklist: hire enough people, plug them into the existing workflow, and assume the machine will hum. But scaling without stress-testing that plan is like driving a new route at night with no headlights. You need to see where the bottlenecks hide before they become traffic jams.
Pull the plan apart before you double down. Simulate a sudden spike in orders or a key team member stepping away for two weeks. Watch where communication breaks, which handoffs stall, and how fast new hires actually reach full output. Those friction points are cheaper to fix now than when you're already stretched thin.
Then adjust the onboarding flow, tighten the documentation, or rethink the role split. A ramp-up plan that survives a few deliberate stress tests will carry you through real chaos without the panic. Test it early, patch the holes, and scaling stops feeling like a gamble.
FAQ
First check whether the factory actually owns its own mold shop and injection molding equipment, not just an assembly line. Ask to see the production floor or a video walkthrough showing how they handle precision domes and contacts. Also ask which industries they have supplied before—medical, automotive, or consumer electronics—because lifecycle and tactile feel requirements vary a lot. Finally, confirm whether their engineering team can offer improvement suggestions at the sampling stage instead of only building to print.
A good sign is that they ask many questions about your operating environment before quoting: actuation force, travel, expected life, dust or water resistance, PCB layout constraints. If they only care about quantity and target price, they will likely just offer a standard model with a different color. Ask for similar application case studies, or have them simulate your pressing scenario for life testing. A factory that truly understands will point out details you may have missed, like dome snap noise or solder joint fatigue.
The difference mainly comes from the mold development process and dome inventory. Some factories outsource molds, and back-and-forth revisions add weeks. Others have an in-house mold department that can work in parallel. Also, the thickness and plating of dome materials like stainless steel or phosphor bronze affect stamping and heat treatment time. If a supplier keeps common dome and base specifications in stock, sampling might take only ten days, while starting from zero can take over a month. Ask about their critical material stock levels.
A real partner gets involved during the design phase, helping you choose the dome curvature, terminal plating, and plastic material, sometimes even suggesting changes to the switch shape to improve soldering yield. Assembly-only companies usually accept only finalized drawings and ask you to change the design after a problem appears. Another difference is how they respond to failures: a partner will proactively analyze whether the cause is incoming material or process-related and provide an 8D report instead of simply sending replacement parts.
It is extremely important. Many hidden costs come from mold ownership. If you pay for the tooling, make sure the contract states that the molds belong to you and can be removed at any time. Otherwise the supplier might use your molds to produce similar parts for other customers, or charge you a high mold storage fee when you want to move production. Also confirm mold life expectancy and maintenance responsibility so you are not forced to pay again if the mold wears out mid-production.
Customization pays off when your product has a special tactile feel requirement, limited mounting space, or needs integrated LED, waterproofing, or extended lifetime. For ordinary consumer electronics, a standard part saves mold cost and time. But note that customization is not always much more expensive, especially if your annual volume exceeds 500,000 pieces—amortized cost per unit can be lower than a standard part. Ask the factory to do a cost comparison analysis before you commit to tooling.
Do not just ask for a defect percentage; that number is easy to polish. Ask what equipment they use to test dome force and travel, and whether they do full inspection or specify a sampling frequency. Request recent in-process inspection records, especially data on dome misalignment and soldering defects. Also ask how they trace and isolate a batch if a systemic issue appears. If possible, get feedback from one or two of their existing customers about real-world quality performance.
Yes, but you need to choose a factory that specifically serves low-to-medium volume customers. Some shops use a common mold base and only change the core to reduce cost, so you only pay for the core. Also, do not squeeze the price too hard at the sampling stage—the factory will recover profit later through material or process choices. For small runs, negotiating a reasonable tiered price for 3k, 10k, and 30k pieces is more practical than chasing the lowest possible unit price.
Conclusion
Choosing an OEM tactile switch factory rarely comes down to a glossy catalog or a low unit price. The partners worth keeping are the ones who show you their engineering bench, not just their shelf. Ask for a custom modification that actually matters—different actuation force, a sealed stem, an alternate terminal—and watch how they respond. A factory with genuine depth will push back with material and tolerance trade-offs, not just say yes. Prototype speed is another honest signal: how quickly they turn a rough napkin sketch into a clickable sample tells you whether their problem-solving is real or rehearsed. And before you commit, pin down tooling ownership. Too many brands assume they own the mold, only to find out later that the tool stays with the factory and your design is effectively held hostage. Get that in writing, including maintenance records and transfer rights.
Certificates on a wall mean little if the floor doesn't live up to them. Walk the line—or ask for video—and look for in-process checks: contact resistance sampling, force curve testing, dust and humidity controls. A factory that can show you real rejection data and corrective actions is a factory that owns its quality, not one that hides behind an ISO badge. Communication rhythm matters just as much. Do they answer with a clear owner for your project, or does every email disappear into a group chat? The cadence of updates, especially when something goes wrong, exposes their true culture. Finally, test their ramp-up plan before you need it. Ask how they handle a tripling order: which lines flex, which suppliers hold buffer stock, what staffing triggers exist. A factory that can walk you through that chaos with calm specifics is one you can scale with—not just survive a single PO.
Contact Us
Contact Person: Anna lin
Email: [email protected]
Tel/WhatsApp: +86 13567768885
Website: https://www.kjele.com/