How an Investment Casting Exporter Delivers Precision Components Worldwide
2026-11-16
A precision component rarely announces itself until it performs—or fails. That is why sourcing teams look beyond price and start asking tougher questions about process control, material traceability, and cross-border reliability. In investment casting, those questions separate local job shops from a genuine investment casting exporter. Supreme Machinery sits firmly in the second category, delivering components that meet exacting standards across aerospace, medical, energy, and industrial markets. This article unpacks how that global capability comes together, from wax patterns and shell building to final inspection and delivery.
From CAD File to Crate Without Losing Microns
Every design begins as a clean digital model, but somewhere between the screen and the shipping dock, precision tends to quietly slip away. The challenge isn't the machining itself—modern CNC equipment easily holds tolerances measured in microns. The real risk lives in the handoff: a slightly misaligned fixture, a worn locating pin, or a conversion that rounds a coordinate by half a thousandth. When the final part is nested into its protective crate, all those invisible compromises have already been locked in. Keeping microns intact means treating the crate not as an afterthought, but as the last stage of the manufacturing sequence.
A practical way to close that gap is to make the crate geometry reference the same origin as the CAD file. Instead of building a generic foam cavity and hoping the part settles correctly, the cradle surfaces are generated directly from the 3D model's critical features. That way, a bore that mattered during milling gets a matching support boss in the packaging. Any drift becomes visible immediately—the part won't seat fully, or a probe check at incoming inspection flags an offset that never showed up on paper. It's a simple idea, but it converts the crate from passive storage into an active verification tool.
There's also a human element that often gets overlooked. When technicians on the shop floor can run a quick go/no-go fit against a crate whose surfaces were milled from the same model they just finished machining, they stop trusting only the printout. They start trusting the physical relationship between part and packaging. That confidence travels all the way to the customer's loading bay. And it costs very little—just the discipline to keep one digital thread unbroken from the first sketch to the final snap of the lid.
Why the Wax Pattern Still Decides What Ships Overseas
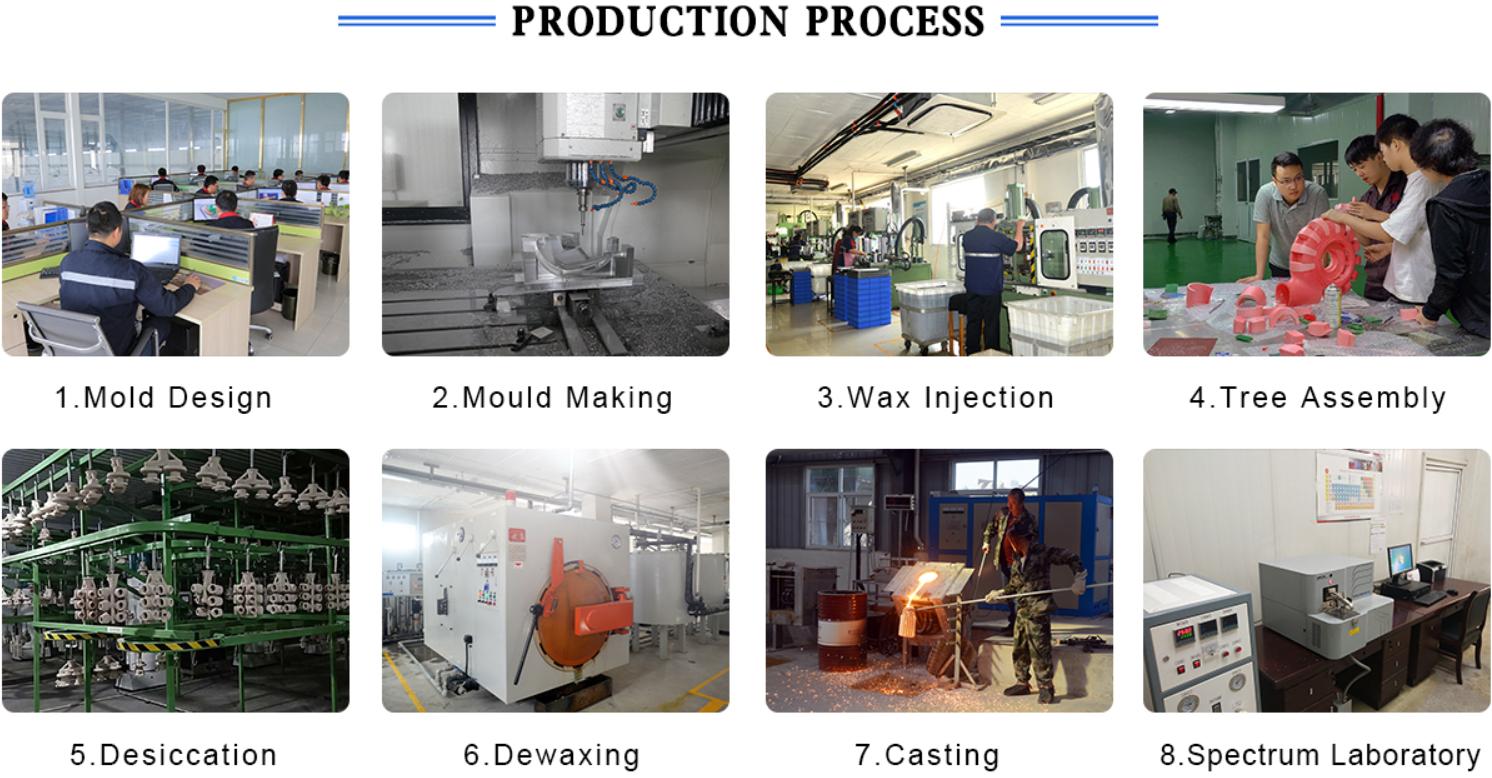
A casting supervisor once put it plainly: the wax pattern is the last honest version of the part before metal hides the mistakes. When a pattern leaves the injection press, every sink mark, crack, or uneven radius is still visible. Once it gets coated in ceramic and burned out, those flaws transfer into the steel or nickel alloy with a fidelity that machining cannot always rescue. That is why the final shipping decision often happens before a single pound of alloy is poured.
The pattern also carries the geometry that matters for downstream operations. Shrinkage allowances, gate placement, and even the way a part will sit in a heat-treat rack are all set at the wax stage. If a pattern shifts by half a millimeter or gets handled too warm, the finished casting may still pass a visual check and then fail a coordinate measuring machine later. Overseas buyers know this, so their incoming inspection starts with the wax record as much as the final dimensional report.
Some newer shops have added blue-light scanners and automated dip lines, but the wax still decides what gets packed because it is the cheapest point to fix a problem. Reworking a wax pattern takes minutes and a few tools; reworking a ceramic shell is a gamble; reworking a shipped casting is a negotiation. That economic order is old, unglamorous, and still very hard to argue with.
The Shell Room Is Where Export Confidence Begins
Confidence in an export shipment rarely starts at the loading dock. It begins earlier, on the wet floor of the shell room where every basket of product is inspected, sorted, and handled under tight time and temperature controls. Small inconsistencies in shell condition, size, or freshness are easier to catch and remove here than they will ever be later in the chain.
The room itself is built around restraint: stainless tables, chilled water, clear bins, and a crew that knows when to stop sorting and start cooling. That discipline carries through to packing and documentation. A buyer may never see the shell room, but the condition of the carton at arrival tells them whether the room was run properly.
That is why the shell room is treated less as a processing step and more as a first audit. Every cracked shell or slow-cooled crate is a future claim. When the room is steady, downstream paperwork, inspections, and transport become far less fragile.
Tolerances That Hold Up Through Customs and Climate
Real dimensional stability gets tested long before a shipment reaches the job site. We tighten critical mating tolerances about half a grade beyond the drawing limit, not for bragging rights, but because a container parked at a tropical port for three days behaves nothing like one stored in a northern warehouse for two weeks. Wooden crates take on moisture, metal parts sweat, and those small movements eat into the clearance that was supposed to be there. Thermal expansion and moisture absorption are treated as part of the tolerance chain from the start, not as an afterthought once a claim lands on the desk.
Customs inspection adds another layer of unpredictability. Goods get opened, shifted, and resealed, with supports sometimes left slightly out of place. If a fit only works in the original untouched state, reassembly after inspection becomes a gamble. We leave a little repeatable assembly room at fragile interfaces and use vapor-proof film to hold the local microclimate steady. Even when a shipment sits in transit days longer than planned, the dimensions stay inside the assembly window.
Arrival does not always mean immediate installation. Materials may sit exposed on a site or in a warehouse, so we cycle same-batch samples from -15°C to 45°C and from 30% to 90% relative humidity. Critical dimensions move less than 0.2 mm through that range, which is not an extreme number, but it is enough to keep installers from reaching for grinders, shims, or a bigger hammer.
Near-Net Shapes for Buyers Who Hate Second Operations
A part that still needs turning, milling, tapping, and grinding after it lands on your dock is not really a finished part—it is a project with extra lead time attached. Near-net shapes come at the problem from the other direction. Instead of hogging a rough blank down to size, the process puts material roughly where it belongs from the start, so the as-formed surface is already close enough to the final envelope. For buyers who would rather skip the second, third, and fourth setups, that changes the conversation from counting machining hours to identifying the two or three surfaces that actually need a light finish pass.
Closed-die forging, investment casting, powder metallurgy, and metal injection molding all handle this differently, but the useful outcome is the same: holes, bosses, recesses, keyways, and even near-final threads can be formed in the tool instead of cut later. That does not mean every dimension comes out inspection-ready. It means the remaining work is narrow enough to schedule around one fixture or one machine, rather than a long routing that bounces between departments. When volumes support the tooling, the savings show up less as a line-item cost cut and more as fewer places for a job to stall.
There is a trade-off, and pretending otherwise does nobody any good. Tooling can be expensive, and not every geometry suits a forming process. But if the alternative is paying for machine time, chip disposal, extra deburring labor, and the scrap rate that comes with all of it, near-net often wins for mid-to-high volume work. The practical question is not whether a process can hit some idealized zero-machining promise. It is whether the part arrives with only the critical fits left to finish—and whether that lets a buyer stop babysitting a routing sheet and start treating the supplier like a source of parts, not problems.
How a Foundry Learns Your Part Better Than Your Drawing Shows
A casting drawing usually captures the intended final shape, but it rarely tells the whole story of how metal will actually behave. In the foundry, engineers look past the nominal dimensions and start reading the part the way a machinist reads tool wear. They notice where a wall thickness shifts abruptly, how a boss connects to a thin web, and which surfaces will be machined later. These observations come from years of watching solidification fronts, shrinkage patterns, and hot tears. The drawing says what the part should be; the foundry learns what the part wants to do while it is being made.
That learning process often begins before the first pour. Simulation tools reveal where the last metal to freeze will sit and whether a riser can actually feed it. Patternmakers adjust draft angles not because the print asks for them, but because they know a deep pocket will drag in the mold. Core setters mark vent locations that never appear on the drawing, yet without them the gas has nowhere to go. Each of these small corrections is a form of knowledge the drawing cannot carry, because it comes from the interaction between geometry, alloy, and process.
Over time, a foundry builds an internal library of what certain features really mean. A hole that looks simple on paper may need a chill behind it to avoid porosity. A flat surface may need a slight crown to stay flat after cooling. The original drawing remains the contract, but the foundry's understanding becomes the method. When that understanding feeds back into tooling, gating, and riser placement, the result is a casting that meets the print not by luck, but by having been read correctly long before the metal arrived.
FAQ
Plenty of buyers think the job ends when parts pass final inspection. In practice, the exporter also manages export documentation, Incoterms, customs classification, consolidated freight, and proof of origin. For a shipment going from a foundry in one country to a machine shop in another, a missing certificate or a vague HS code can hold the container for days. A good exporter keeps those paperwork details moving in parallel with production so the physical parts and the documents arrive together.
The casting process has to be planned with the next step in mind. We leave controlled stock on surfaces that will be machined later, and we record shrinkage rates by material and section thickness instead of applying one generic allowance. For parts that get measured overseas, we include a small dimensional report with the exact datums used, so the receiving shop is not guessing where the part was held during inspection.
Valve and pump manufacturers, food processing equipment builders, agricultural machinery makers, and specialty automotive suppliers are the most common. Medical and aerospace work also moves across borders, but it usually comes with extra audit requirements and tighter paperwork. The common thread is that the buyer needs a shape that would be expensive to machine from solid stock or difficult to fabricate in-house.
Stainless steels, carbon steels, low-alloy steels, and many copper-base alloys are routine. High-nickel and cobalt alloys can still be shipped, but they may need additional declarations depending on the destination and end-use. The real issue is not usually the alloy itself; it is whether the buyer has clearly identified the final application. A vague description like industrial equipment parts can trigger more questions than a specific description like pump impeller for water treatment.
We build the schedule around the shipment date, not the casting date. That sounds small, but it changes how capacity is reserved. If a vessel is booked for the third week of the month, we work backwards and reserve furnace time so that finishing and inspection are done a few days before the container cutoff. We also separate long-lead raw materials early, because alloy availability causes more delays than customs in many cases.
Yes, but the tooling strategy is different. For prototypes, we may use a lower-cost tool or a 3D-printed pattern to validate the geometry before committing to a high-volume die. Once the design is stable, we move to a production tool that can handle repeated wax injections without losing detail. The casting parameters stay the same; only the upstream tooling and the inspection frequency change.
A lot depends on the end use. Parts that will be machined later should arrive clean but not over-polished, with machining stock intact and protected from dings. We use partitioned foam, VCI paper for ferrous alloys, and sealed bags for parts going into humid climates. For finished components, we might add passivation or a light oil film and then pack by part number so the buyer does not have to sort mixed boxes on arrival.
Each heat is tied to a cast lot number, and that number follows the parts through shell building, pouring, finishing, and inspection. We provide mill certificates for the raw material and a separate chemical and mechanical test report for the cast parts when required. If the buyer needs third-party verification, we can arrange inspection before shipment, but the default is a traceable lot structure that lets the customer pull up one heat and see every process step attached to it.
Conclusion
An investment casting exporter doesn’t ship hopes; it ships controlled shrinkage. The work starts with a customer’s CAD file, but that file only becomes useful after tooling and process planning account for every place the part could move before it lands in a crate. A few microns lost in wax injection or pattern assembly follow the part through shelling, pouring, and finishing. That is why the wax pattern still decides what goes overseas. If the pattern is not straight, stable, and lightly handled, no amount of downstream inspection can put the tolerance back. Tooling is cut so dimensions survive long hauls, humid ports, and rough handling without turning a good casting into a rejection.
Export confidence is built layer by layer in the shell room. Each slurry dip and stucco coat has to match the alloy and section thickness, because the shell is what keeps metal sound while it solidifies thousands of miles from the customer’s shop. Buyers who order across borders rarely want to chase second operations, so near-net geometry matters. A foundry that does this well learns where a part flexes, where stock is unnecessary, and which datums are actually functional—sometimes better than the drawing shows. The result leaves the dock ready to fit, not ready for another shop visit.
Contact Us
Contact Person: Paul
Email: [email protected]
Tel/WhatsApp: 8615067447509
Website: https://www.spironcasting.com