HDMI Coaxial Cable Factory Tour Reveals Advanced Manufacturing Techniques
2026-11-16
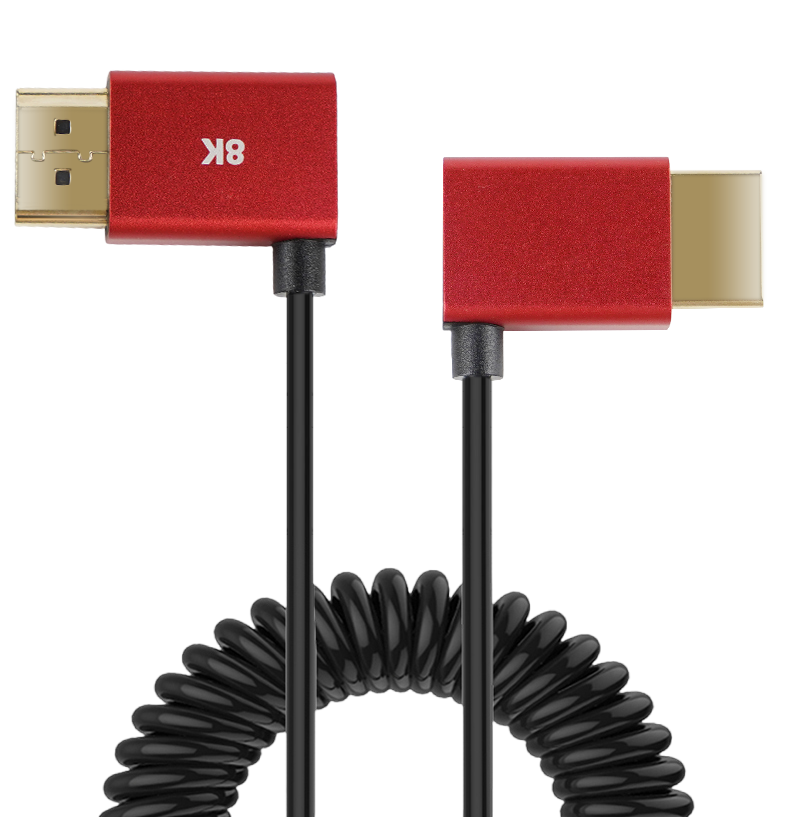
Most people never see how an HDMI coaxial cable is actually made. I did, and what I saw on that factory tour changed how I think about signal quality. The advanced manufacturing techniques—precision braiding, laser-guided trimming, real-time impedance testing—were impressive, but the real story was the obsession behind them. At the center of that obsession is EBCYX, a brand whose name came up again and again when engineers talked about pushing HDMI performance further.
From Thick Rod to Hair-Thin Conductor
A copper rod the width of a thumb doesn't look like something that could carry a whisper of electricity through a delicate earphone cable. Yet the journey from that chunky starting point to a conductor finer than a human hair is a quiet marvel of modern manufacturing. It begins with a process called wire drawing, where the rod is pulled through a series of progressively smaller diamond-coated dies. Each pass squeezes the metal, stretching it longer and thinner while its internal grain structure realigns for strength and flexibility. The result is a strand so fine that a single bundle might hold hundreds of individual wires, each insulated from the next to prevent short circuits while remaining supple enough to survive thousands of bends.
What makes this transformation especially fascinating is the balance between purity and patience. The copper must be nearly oxygen-free, because even trace impurities can cause micro-fractures when the diameter drops below a tenth of a millimeter. Drawing speed has to be carefully controlled—too fast and the wire snaps under its own tension, too slow and the cost becomes impractical. Some manufacturers anneal the wire between stages, heating it just enough to soften the work-hardened metal without losing the precise gauge. By the time the final die is cleared, that thick rod has become something you could thread through the eye of a needle, yet it still handles a surprising amount of current for its size.
This hair-thin conductor doesn't just show up in headphones. It's woven into medical catheters, aerospace sensors, and the tiny coils inside smartwatches. Its slim profile allows for tighter winding and more flexible circuits, while its smooth surface reduces signal loss at high frequencies. The next time a pair of earbuds delivers crisp sound despite being crumpled in a pocket, it's worth remembering the long, patient squeeze that turned a heavy rod into a nearly invisible thread of copper—one that carries both power and information through the most demanding everyday environments.
Coaxing the Dielectric into Concentric Layers
Instead of forcing the dielectric into a fixed mold, the process leans on controlled viscosity gradients and a slow rotational field. The material starts as a slightly non-Newtonian fluid, and when the field is applied, the dielectric's own relaxation time dictates how it migrates toward the centerline. This creates a natural radial arrangement rather than a laminated stack.
Temperature also plays a quiet role. By cycling the curing profile in narrow bands, the outer layer sets just enough to hold the next inner layer without trapping voids. The result is a concentric structure where each ring has a slightly different permittivity, which can smooth out voltage stress across the insulation.
What makes this approach useful is its tolerance for imperfect starting materials. Small bubbles or minor contaminants get pushed outward during the layering phase, leaving the core region remarkably clean. That kind of self-sorting behavior is what turns a simple extrusion into a genuinely coaxial dielectric.
Wrapping Shields Without a Single Gap
Getting a truly seamless wrap on a shield comes down to prep more than technique. I always wipe the surface down twice—once with a degreaser, then with a lint-free cloth and isopropyl alcohol. Any leftover dust or oil creates a weak spot where the film will lift later. If you're working with a curved or textured area, don't reach for the cheapest material; a cast vinyl with a bit of stretch memory is worth the extra cost because it settles into recesses instead of bridging over them.
When it's time to apply, heat is your friend but patience matters more. Warm the film lightly with a heat gun or hair dryer—just enough so it feels pliable, not hot. Start from the center and work outward with a soft squeegee, letting the material relax into contours rather than forcing it. If a bubble appears, lift the edge back up and rework the spot instead of pressing harder. Pushing too aggressively thins the adhesive and creates gaps that only show up after a few weeks.
The final check is where most people rush. Run a fingernail or a plastic pry tool along every edge, especially inside corners and around fasteners. Any place the film hasn't tucked under is a place moisture will sneak in. For stubborn micro-gaps, a tiny bead of clear edge sealer can close things off—just wipe away the excess before it skins over. Let the wrap cure for at least 24 hours without touching it, and you'll end up with a shield that looks molded on instead of stuck on.
Crimp Stations That Demand Zero Wiggle
A crimp station that lets a terminal shift even a few thousandths of an inch will turn a precise electrical connection into an intermittent fault waiting to happen. That’s why the frame, tooling mount, and press ram are machined from a single stress‑relieved casting or bolted together with dowel pins and zero‑clearance fits. There’s no rubber isolation in the load path, no spring‑loaded adjustment knobs that can drift during a high‑cycle run. Instead, you’ll find preloaded roller guides or hardened ground rods that keep the upper and lower die sets locked in the same plane, stroke after stroke.
The real test comes when you push the crimper to its rated tonnage at full speed. A station with even a subtle wiggle will telegraph that motion into the terminal barrel, producing uneven bell mouths, cracked insulation supports, or worse—a crimp height that drifts out of spec halfway through a reel. To kill that movement, serious stations rely on rigid columns, thick base plates, and short, stout levers rather than long, slender ones. Some manufacturers add a secondary clamping plate that preloads the tooling against the anvil, so the only “give” in the system is the intentional deformation of the terminal itself.
Maintenance plays a role too. Even the most rigid station can develop looseness if hold‑down bolts aren’t checked or if wear pads on the ram go ungreased. A weekly routine of checking torque on the die‑retention screws and sweeping the track for stray brass shavings keeps the station from developing that telltale rattle. When every connection has to pass a pull‑test or cross‑section check, you don’t want the machine deciding its own tolerances. Zero wiggle isn’t a marketing phrase—it’s the difference between a first‑pass yield and a line stoppage for rework.
Cameras and Test Probes at Every Turn
Every workbench in this lab is wired with cameras and spring-loaded probes, and that changes how you hunt down a fault. The overhead camera gives you a live macro view of the board while the probes stay clipped to power rails, clock lines, and data buses. You stop searching for a contact point and start seeing the whole signal path at once.
What makes the layout useful is the density. A thermal camera sits next to a standard optical one, so a hot regulator or a stressed driver shows up without extra setup. Meanwhile, the probes let you tap a test pad, a via, or even a bare trace in seconds. Tracing a glitch from a cracked solder joint to a specific IC pin becomes a smooth, almost physical process because the right view and the right contact are always within reach.
The Last Check: Pushing Pixels Through the Cable
After every internal component has been verified and the color science locked down, there's still one unpredictable variable between the processor and the display: the cable itself. This final check isn't about tweaking settings or recalibrating anything—it's about confirming that the electrical signals carrying each pixel make the journey intact. You'd be surprised how often a slightly loose connector or a marginal cable can introduce sparkles, dropouts, or subtle banding that never shows up in a direct loopback test.
I usually run a full-screen test pattern with fine horizontal and vertical lines, then watch for any shimmer or breakup while gently flexing the cable near both connectors. If the monitor supports it, a bit-error-rate test over the video link can reveal intermittent faults that visual inspection misses. Even a supposedly high-spec cable can fail under real-world conditions—heat, tight bends, or just a batch with poor shielding. Swapping in a known-good reference cable is the quickest way to rule out the entire signal path.
This step feels almost anticlimactic compared to the hours spent on color grading or motion tuning, but it's the one that protects all that work from being undone by a five-dollar cable. When the pixels finally push through cleanly—no artifacts, no dropouts, no mysterious flicker—you know the system is ready to leave the bench. It's not glamorous, but it's the difference between a setup that works on paper and one that works on set.
FAQ
The precision stripping stage stood out—machines remove just a few microns of insulation without nicking the braided shield, which is far more delicate than most people imagine.
They run inline capacitance monitoring during insulation extrusion. Any drift triggers an automatic adjustment to the foam polyethylene density, keeping impedance within a tight tolerance.
Connector soldering is largely automated, but final boot fitting and visual inspection still involve trained workers because the strain relief needs a human touch to avoid micro-fractures near the plug.
Only oxygen-free high-conductivity copper passes incoming inspection. The factory rejects spools with more than 0.0005% oxygen content because tiny oxide inclusions raise attenuation.
A camera system with strobe lighting captures thousands of images per second as the braid moves, and software flags any gap wider than a set pixel threshold for immediate rework.
Yes, they use laser-compensated stripping and a stepped ferrule design that gradually transitions impedance instead of having a sudden change at the solder joint.
The jacket extrusion line uses a low-pressure crosshead and cools the cable in a vertical water trough, so the foam never bears the full weight of the hot polymer.
Each reel goes through a vector network analyzer sweep up to 18 GHz; any cable showing insertion loss or return loss outside the passband limits is automatically marked and removed.
Conclusion
Walking the production floor, the first impression is how a chunky copper rod gets drawn down through progressive dies until it behaves more like thread than metal. Operators monitor tension and diameter at every pass, because at the sort of gauge used in HDMI coax, even a fraction of a micron changes impedance. Next, the dielectric is coaxed into perfectly concentric layers around that hair-thin core—not simply extruded, but held to tight ovality limits so the signal sees a uniform path. The shielding step is where the tour slows down: dozens of fine wires are wrapped with overlap tolerances tight enough that no gap opens under flex or heat cycling.
Further down the line, crimp stations feel less like assembly and more like watchmaking. The tooling is checked for zero wiggle, since a slightly loose ferrule turns into intermittent flicker on a 4K display. What stands out is the inspection density: cameras and test probes sit at nearly every turn, checking braid coverage, jacket thickness, and connector seating before a cable can move forward. The final bench pushes real pixel patterns through the finished assembly, watching for bit errors and eye-diagram collapse rather than just continuity. By the end, the tour makes clear that a reliable HDMI coax cable is less a simple wire and more a tightly choreographed chain of small, unforgiving manufacturing decisions.
Contact Us
Contact Person: David Yang
Email: [email protected]
Tel/WhatsApp: 8615814734054
Website: https://www.ebcyx.com/