China OEM AS/RS Warehouse Pallet Factory for Automated Storage Efficiency
2026-10-13
If you've ever walked through a distribution center and wondered how thousands of pallets move without a single forklift in sight, you've glimpsed the quiet power of an AS/RS system. At Lanyuda, our OEM warehouse pallet factory in China doesn't just assemble steel frames—we engineer the backbone of automated storage efficiency. This isn't about stacking boxes; it's about reshaping how warehouses breathe, move, and scale.
Inside the Welding Bays Where AS/RS Pallets Take Shape
Stepping past the yellow safety line, the first thing that hits you is the staccato crackle of MIG torches—not the steady roar you might expect. Each bay is a loose choreography of overhead cranes, turntables, and steel jigs worn smooth at the corners. A pair of welders works opposite ends of a pallet frame, laying short stitch welds in a sequence that fights distortion before it can take hold. The air carries that sharp, metallic tang of ozone mixed with grinding dust, and underfoot the concrete is scattered with tiny silver spatter beads that crunch like coarse sand.
What separates these bays from a typical structural welding shop is the obsession with flatness and squareness. An AS/RS pallet doesn't just sit on a rack; it has to interface with automated shuttles that measure positions in millimeters. Even a 3-mm bow across a 2-meter span can cause a retrieval arm to fault out or a load to shift during high-speed travel. So the jigs here aren't just holding fixtures—they're actively clamping, pre-cambering, and sometimes water-cooling the frame while the weld sequence moves from center outward. It's a slower process than it looks, and the best welders know when to pause and let the steel breathe.
Toward the back of the bay, finished pallets wait in a queue, each tagged with a heat number and the initials of the welder who ran the final pass. A quality tech runs a straightedge across the top face and checks diagonal measurements with a laser, but most of the real assurance happens earlier—in the tacking order, the root gap, the way a welder feathers the start of a bead to avoid a hard toe line. It's that blend of old-school torch control and stubborn dimensional discipline that keeps AS/RS pallets from becoming the weak link in an otherwise automated warehouse.
OEM Orders That Follow Your Spec, Not the Other Way Around
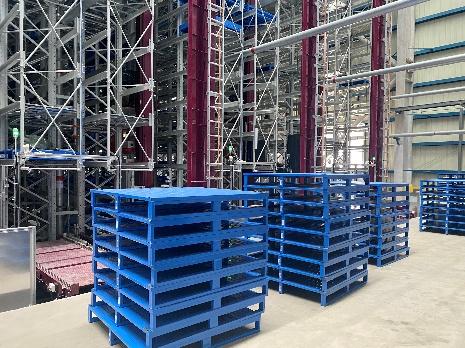
Your drawings, tolerances, and material choices drive everything we do. We don't ask you to adjust your design to fit our equipment—instead, we adapt our tooling, fixturing, and processes to match what you've specified. Whether it's an unusual thread pitch, a tight flatness callout, or a non-standard surface finish, those details are locked in before the first cut.
Small batches with exacting specs? No problem. Our engineers review every RFQ against your technical package and flag potential issues before they become costly surprises. From raw stock selection to final inspection, each step is checked against your print, not a generic checklist. If a dimension doesn't hold, we don't ship—we rework or start over.
You stay in control through the entire run. We send dimensional reports and photos at key milestones, so you can verify conformance without waiting for a final shipment. And if a last-minute revision comes in? We pivot fast, updating CNC programs and setups without treating your change as a disruption. That's what it means to follow your spec, not the other way around.
How Stiffer Frames Cut Automated Retrieval Downtime
When retrieval systems jolt to a halt, the culprit often hides in the frame. A stiffer frame absorbs less vibration during high-speed operation, keeping sensors and grippers aligned within tighter tolerances. That stability means fewer micro-collisions, fewer false reads, and far less time spent chasing intermittent faults.
Frames with higher torsional rigidity also resist the slow creep of misalignment that builds up over thousands of cycles. Once the framework stops flexing, the whole motion profile becomes more predictable. Maintenance teams can then shift from reactive fixes to planned inspections, cutting unplanned downtime dramatically.
The real difference shows up in environments with rapid direction changes or heavy end-effectors. A rigid backbone lets the control system trust its own commanded positions instead of constantly compensating for deflection. That extra confidence translates directly into longer runs between interventions and a smoother overall retrieval workflow.
Material Choices That Outlast Constant Shuttle Traffic
High-density nylon and polypropylene blends remain the quiet workhorses in corridors that see rolling suitcases, service carts, and endless footsteps. Look for solution-dyed fibers rather than piece-dyed ones—color locked through the strand resists fading and hides scuffs far better when wheels grind against the same stretch day after day.
For hard surfaces, specify porcelain tile with a PEI rating of IV or higher, or opt for polished concrete treated with a lithium-based densifier. These materials shrug off the constant abrasion without developing visible wear paths, and their low porosity means spilled coffee or tracked-in grit won't become permanent stains. Rubber sheet flooring with heat-welded seams also earns its place in tight, high-traffic zones because it absorbs impact quietly and never needs waxing.
Pallet Profiles for Every Aisle Width and Load Curve
Warehouse managers are often forced to choose between narrow aisles and heavy throughput. A well-designed pallet profile removes that compromise. By repositioning the pallet feet or bottom deck boards, the pallet can navigate a tight turning radius while still offering enough contact surface to distribute a dense load. This isn’t about making a pallet smaller—it’s about shaping the underside so clearance and stability work together rather than against each other.
Load curves vary sharply by industry. A beverage pallet might concentrate weight near the center, while automotive parts spread pressure more evenly across the full footprint. Tailoring the pallet profile to these patterns means placing reinforcement ribs where the stress actually lands, not uniformly across the bottom. The result is less material waste and a stiffer structure that resists sagging under repeated cycles, even when aisle clearances force handlers to place pallets at slight angles.
From narrow-aisle reach trucks to automated shuttle systems, the available clearance dictates how much room a pallet has to rock, shift, or flex. Matching the pallet profile to both the aisle constraint and the load distribution reduces edge damage, improves stack stability, and extends service life. This level of granular design used to be reserved for high-volume orders, but parametric modeling now makes small-batch customization economically viable—so even a single warehouse zone can run pallets shaped for its exact operating envelope.
Shipping From Our Floor to Your Rack Without a Forklift Mishap
We take the guesswork out of getting heavy equipment from our dock to your storage area. Each unit is strapped, padded, and positioned on the pallet so the center of gravity stays low—no wobble when a forklift slides under it.
Our crew checks every load against a simple diagram before it leaves the floor. If a pallet doesn't sit dead level or a strap shows wear, it gets rebuilt right then, not at your loading bay.
When the shipment arrives, the same care continues. The skid is marked with lift points, and the underside is kept clear of loose wrap, so your forklift operator can take it straight off the truck and into the rack without repositioning or last-minute corrections.
FAQ
The focus is on pallets built for automated storage and retrieval systems. These are not off-the-shelf warehouse pallets - they are designed around the exact travel paths, lift heights, and shuttle interfaces of AS/RS equipment.
We start with your equipment's interface drawings or, if those are not available, a site survey of the rack and shuttle dimensions. From there we adjust pocket spacing, rail guides, and load-bearing points so the pallet seats and moves correctly in your specific system.
Most orders use structural steel with a powder-coated finish, but we can switch to galvanized steel, aluminum, or even add anti-slip rubber strips if your product or environment calls for it. The choice depends on load weight, humidity, and frequency of retrieval.
Dimensional checks happen at three stages: after laser cutting, after welding, and after final coating. We hold flatness to within 2mm across the pallet surface and check all edge radii against the shuttle's minimum clearance requirements, so there is less chance of catching or misalignment.
For a new design, expect 25 to 35 days from drawing approval to shipment. If you are reordering an existing design we have already tooled up for, that can drop to 15 to 20 days.
Yes, we run finite element analysis on every custom design. You give us the maximum pallet load, how it is distributed, and whether the pallet sits static or gets lifted by forks or conveyors, and we will confirm the required steel thickness and rib placement.
Our current capacity is around 3,000 to 5,000 pallets per month depending on size and complexity. For very large orders we can reserve dedicated production lines to keep the output consistent.
Conclusion
The AS/RS pallets leaving our factory don't begin as generic rack decks. They're cut, fixtured, and welded in dedicated bays where each order gets its own setup based on the aisle width, shuttle type, and load curve the customer sends over. That OEM-first approach means things like corner gussets, cross-brace spacing, and fork pocket placement follow your automation interface rather than forcing you to adapt to a stock design. We also add extra rigidity in the frame rails and top plates, because even a few millimeters of flex under high-speed retrieval can throw off positioning sensors and cause the shuttle to fault out. A stiffer pallet stays predictable over thousands of cycles.
Material choices matter just as much as the weldments. Where shuttle wheels and transfer rollers ride constantly, we use thicker edge profiles and abrasion-resistant coatings so the contact surfaces don't groove or peel into raised lips that snag the load. We can profile the pallet deck and runners to match everything from narrow-aisle deep-reach systems to wide-load unitized racks, keeping deflection within your spec. Once the pallets pass final inspection, they're blocked, strapped, and loaded with the fork pockets aligned to your rack entry and the stack height marked clearly, so arrival at your dock doesn't turn into a forklift repair job.
Contact Us
Contact Person: Johnny
Email: [email protected]
Tel/WhatsApp: +86 18151010686
Website: https://lydstorage.com