Best Rubber Conveyor Belt Vendor from China for Durable Industrial Solutions
2026-09-04
Finding a reliable rubber conveyor belt vendor can make or break your industrial operation. When downtime costs thousands per hour, you need a supplier that delivers durable solutions, not just promises. That’s why many procurement teams are turning to XAN, a proven Chinese manufacturer known for belts that withstand extreme loads and harsh environments. In this post, we’ll explore what sets their products apart—from reinforced carcass designs to custom compound formulations—and why sourcing from China no longer means compromising on quality.
Why Chinese Conveyor Belts Dominate Heavy-Duty Applications
A decade ago, the heavy-duty conveyor belt market leaned on European and Japanese suppliers for critical mining and port operations. That balance has shifted, and the reasons go well beyond sticker price. Chinese manufacturers now run some of the largest continuous vulcanization lines in the world, capable of producing single-roll belts over 400 meters long at widths up to 2,400 mm. This reduces field splices, which are the weak points in any high-tension system. On the material side, domestic R&D teams have moved from reverse-engineering foreign compounds to formulating their own high-abrasion rubber blends using locally sourced synthetic rubber and modified carbon black. These compounds are tested against DIN and ISO standards, and in many cases exceed the abrasion resistance offered by legacy European grades under identical load conditions.
Vertical integration also plays an outsized role. Many plants control everything from steel cord drawing and fabric weaving to rubber mixing and final curing under one roof. That cuts logistics waste and lets engineers adjust tensile strength or cover thickness mid-production without waiting on external suppliers. The result is a belt that can be tailored for specific mineral loads, whether it’s sharp copper ore or abrasive iron tailings, without the multi-month lead times that used to plague imported options. Combined with automated inspection systems that scan for cord spacing and cover defects in real time, Chinese heavy-duty belts now compete on consistency and lifespan rather than simply undercutting on cost.
Selecting the Right Rubber Compound for Abrasion Resistance
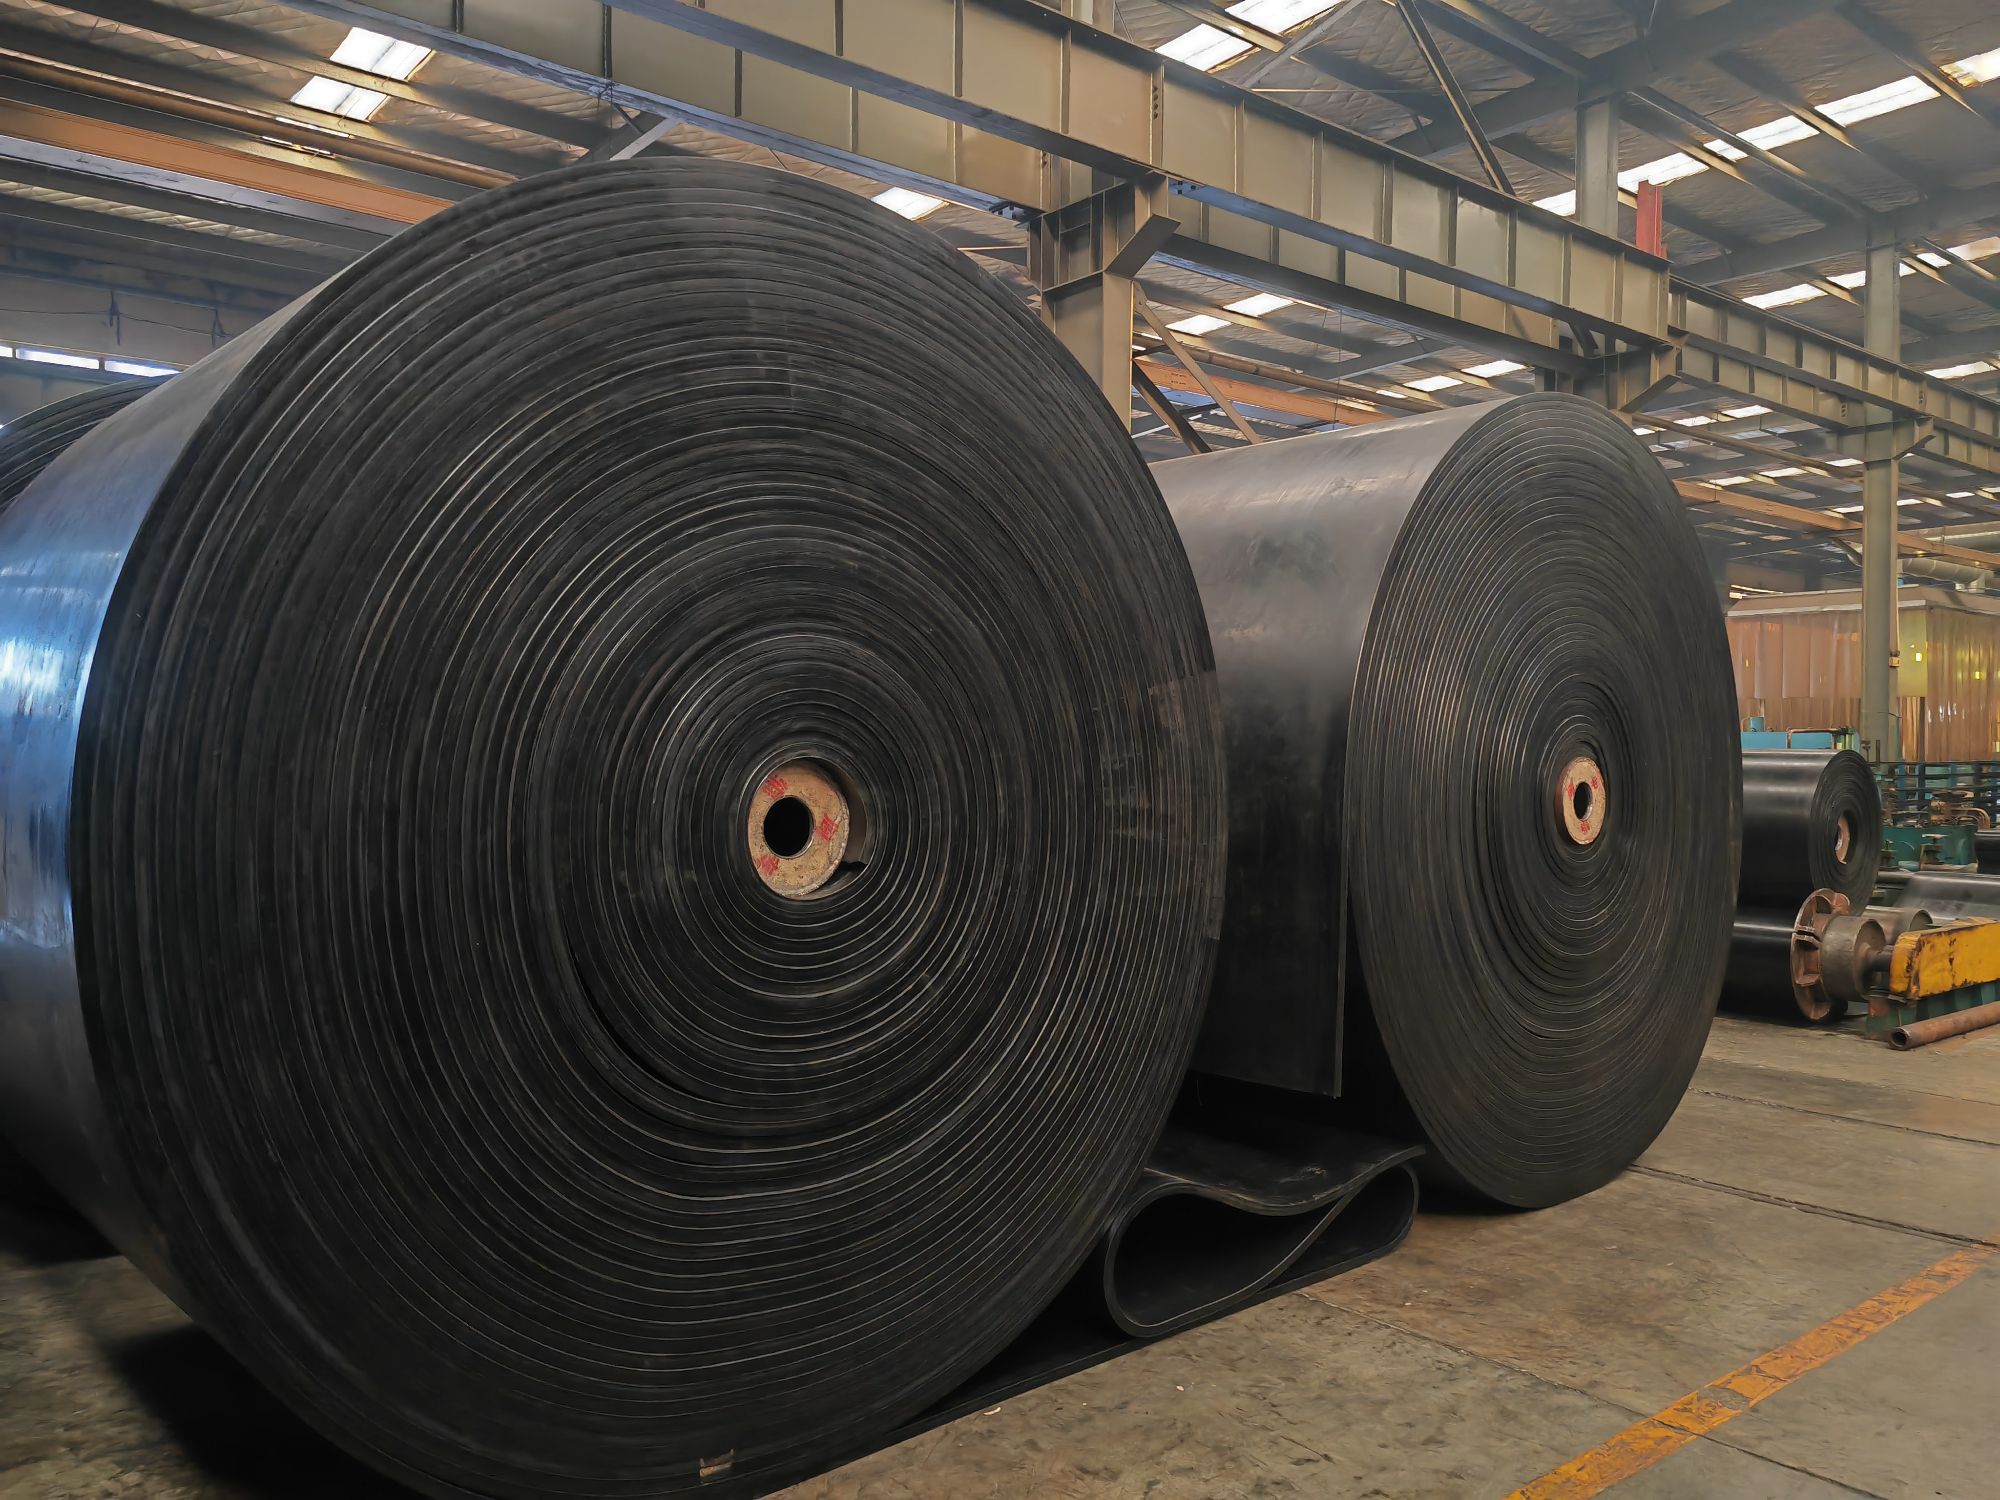
Abrasion resistance rarely comes down to a single material property. Hardness, tensile strength, and elongation all interact, and chasing one often sacrifices another. For example, a very hard rubber may resist cutting but can crack under repeated impact, while a softer compound absorbs energy yet wears quickly on rough surfaces. The real task is matching the wear mechanism to the compound's behavior under the specific load, speed, and temperature conditions the part will face.
Fillers and curing systems shift the balance more than base polymer choice alone. Carbon black grades with smaller particle size and higher structure typically improve abrasion resistance, but only if dispersion is thorough. Sulfur-cured natural rubber often outperforms many synthetics in dynamic abrasion due to its tear strength and fatigue resistance, yet for wet or chemical exposure, a specialty compound like carboxylated nitrile may be the better call. Testing on the actual surface texture and debris type matters more than generic lab numbers.
Field failure usually points to a mismatch in expectations rather than an inferior formula. A compound selected purely by its abrasion index from a data sheet can fail because the real-world wear includes heat build-up, edge nicking, or adhesive transfer. Prototyping with small batches under production-like conditions reveals how the rubber responds to the exact grit, pressure, and sliding pattern. Without that step, even a high-rated compound becomes an expensive guess.
Custom Belt Fabrication That Matches Your Exact Specifications
Every dimension on your drawing gets treated as a hard number, not a suggestion. Tooth profile, pitch, width, length, backing material, cord type, and even the exact durometer of the rubber compound are matched to your file or physical sample. We keep a library of uncommon profiles and can reverse-engineer worn belts when no print exists, so the replacement runs true on the original pulleys.
Fabrication starts with a CAD check of your geometry, followed by laser cutting or CNC grinding depending on the profile. Tolerances are held to ±0.1 mm on pitch and ±0.5 mm on overall length unless your spec calls for tighter numbers. Before any belt ships, it gets pulled on a test rig at working tension while we record elongation, tracking, and tooth engagement. If something looks marginal, we flag it and ask before cutting the full batch.
You do not pay for a catalog part that almost fits. Each order is documented with a material certificate and a dimension report tied to your job number. Short runs and one-offs are standard, and repeat orders match the first article so you can swap belts without re-tensioning or re-aligning the drive.
How Quality Testing Prevents Costly Downtime
Every hour of unexpected downtime drains revenue, erodes customer trust, and forces teams into firefighting mode. Quality testing acts as a shield against these disruptions by catching defects long before they reach production. Rather than waiting for a failure to surface after deployment, rigorous functional, performance, and regression tests expose hidden weaknesses in code, infrastructure, and integrations. This proactive approach turns potential disasters into routine fixes, keeping systems running smoothly and sparing businesses from the high price of emergency repairs.
Beyond simply finding bugs, thorough quality testing reveals how components behave under stress. Load testing simulates peak traffic to identify bottlenecks that could crash a server during a product launch. Security testing probes for vulnerabilities that hackers might exploit to take services offline. Compatibility testing ensures updates don't break existing workflows on older devices or browsers. By validating these edge cases early, organizations avoid the cascading effects of a single point of failure—a database lockup, an API timeout, or a memory leak that silently degrades performance until it triggers a full outage.
The most overlooked benefit is the confidence gained from a well-tested release. When every build passes a battery of automated and manual checks, engineers can deploy without fear. That confidence reduces rushed patches and hotfixes, which are themselves common sources of new downtime. Instead of scrambling after a bad update, teams maintain a steady rhythm of safe, incremental improvements. In the end, quality testing isn't a cost center—it's the cheapest insurance against the kind of downtime that can sink a product's reputation overnight.
Balancing Price and Longevity in Industrial Conveyor Systems
Industrial buyers often make the mistake of equating a low sticker price with savings, yet conveyor systems that fail early from cheap rollers or thin belt covers rack up costs through unplanned downtime. The real lever sits in component selection: a slightly thicker abrasion-resistant top cover on the belt or a bearing with better seal integrity can add months of service life without pushing the price into premium territory. It’s about knowing which upgrades return multiples and which are just marketing fluff.
Maintenance habits amplify this balance. A conveyor that gets routine tension checks and timely replacement of wear strips will outlast a pricier unit left to run until failure. Many plants find that standardizing on a mid-tier belt with scheduled splice inspections beats chasing the cheapest option year after year, because each replacement triggers labor and lost production that never appears on the purchase order.
When comparing quotes, shift the conversation from upfront cost to cost per ton moved over five years. Ask suppliers for realistic wear life estimates under your specific load and speed conditions, then run the numbers yourself. Some operations discover that a 20% higher belt price yields a 40% longer replacement interval, making the "expensive" option the frugal choice in the long run.
Proven Performance in Mining, Cement, and Port Operations
Heavy dust, constant vibration, and round-the-clock duty cycles are everyday realities in mining and cement plants. Our drive systems have been installed in dozens of aggregate quarries and clinker lines, where they keep conveyors, crushers, and mills moving without unplanned stops. One copper mine in northern Chile logged over 40,000 operating hours on a single gear unit before its first major service, a figure that speaks to the robustness built into every component.
For port operations, salt spray and sudden load spikes from ship unloaders or stacking reclaimers demand a different kind of toughness. Our enclosed drive packages use a multi-stage sealing system and corrosion-resistant coatings that have proven effective on quay cranes in Singapore and bulk terminals in Rotterdam. The result is fewer greasing intervals and no seized bearings, even after years of exposure to marine air.
Rather than offering a one-size-fits-all product, we adapt the internal gearing and cooling method to each site's actual load profile. This approach cuts commissioning time and lets maintenance teams plan overhauls around vessel schedules instead of reacting to breakdowns. That practical, field-driven engineering is why operators in these three sectors keep coming back.
FAQ
A good belt combines high-tensile synthetic carcass, abrasion-resistant rubber compounds, and reinforced edges. Look for suppliers that test for tear strength and offer options like flame-retardant or oil-resistant covers.
Request sample sections for abrasion testing, check tensile strength ratings such as EP or NN fabric layers, and ask for third-party lab reports. Reputable vendors often share data on elongation and cover hardness.
Beyond width and length, you can specify cover thickness, ply count, cleat profiles, sidewalls, and special compounds for heat, cold, or chemical exposure. Some suppliers also offer belt edge sealing and pre-spliced loops.
Yes, if you choose heat-resistant grades with EPDM or SBR covers rated for continuous temperatures up to 150°C or higher. Always state the peak and continuous temperature range to the supplier.
Multiply fabric belts are flexible and easier to splice, suitable for medium-length conveyors. Steel cord belts offer higher tensile strength and low elongation for long overland or high-load applications.
Good vendors provide installation guidance, splice kits, on-site training for maintenance teams, and stock common sizes in local warehouses. Some offer belt monitoring sensors as an add-on.
Many export-oriented manufacturers follow ISO 14890, DIN 22102, or AS 1332 and can provide certificates for flame resistance and static conductivity when required.
Lower labor and raw material integration often reduce prices 20-40% compared to Western brands, but insist on detailed material specifications to avoid underestimating total cost per ton conveyed.
Conclusion
Chinese conveyor belt manufacturers have become the backbone of heavy-duty material handling across global industries, and for good reason. The right vendor combines deep expertise in rubber compounding—selecting abrasion-resistant formulations that extend service life under punishing loads—with the ability to fabricate belts to exact widths, thicknesses, and cover grades. Rather than relying on off-the-shelf products, serious buyers work with factories that perform rigorous quality testing at every stage: tensile strength, adhesion, and dynamic fatigue checks that prevent the kind of unexpected belt failure which triggers costly downtime in mines, cement plants, and port terminals.
What separates a durable industrial solution from a budget compromise is not just low upfront cost, but the balance between price and longevity. Proven performance in these demanding environments comes from vendors who understand that a conveyor belt is not a commodity, but a critical system component. They engineer belts that survive sharp aggregate impacts, resist ozone cracking in coastal ports, and maintain tracking stability under continuous operation. Choosing the best rubber conveyor belt vendor from China means securing a partner whose belts deliver measurable reductions in maintenance hours and unplanned shutdowns, ultimately protecting your production schedule and bottom line.
Contact Us
Contact Person: Anna Lu
Email: [email protected]
Tel/WhatsApp: 8618561668850
Website: https://www.x-conveyor.com